If you’re in the injection molding game, you’ve probably heard the phrase “time is money” thrown around more times than you can count—but let me tell you, it’s not just a corporate buzzword. Every second a molding machine sits idle, every cycle that drags on longer than it needs to, that’s cash you’re leaving on the table. A few years back, I was chatting with a production manager at a small auto parts shop, and he was complaining his old vertical molding setup was running three shifts just to meet demand for a simple plastic clip—turns out, he was running a standard two-platen machine that had to fully open, eject parts, and re-close before each cycle, wasting so much downtime. That’s when we started leaning into rotary table injection molding machines, and seeing the switch totally flip his production numbers? That’s why I’m here today to break down exactly how these machines crank up efficiency, no fancy jargon required. Rotary Table Injection Molding Machine

First off, let’s cut through the confusion: a rotary table molding machine isn’t some overcomplicated industrial mystery. It’s got a big, circular, rotating platen—think of it like a round pizza tray, but for molds—that spins between the fixed injection unit and the clamping unit. Most people don’t realize the biggest win here is that it splits the mold into separate stations, right? Like, one station is for the actual injection of molten plastic, and the others are for all the stuff you have to do after the part is molded: ejecting it, trimming excess plastic (that’s called flash, for anyone new here), maybe even inserting metal inserts or labels before the next cycle.
Wait, let’s compare that to a standard machine. On a typical two-platen press, when the mold opens, you have to stop everything—wait for the platen to slide all the way back, grab the part, clean the mold, load any inserts, then close it back up to do the next shot. That’s maybe 10 to 15 seconds of dead time per cycle? Multiply that by 10,000 cycles a day, and that’s over 40 hours of downtime a week—wasted time, wasted energy, missed deadlines. On a rotary table machine? The injection unit stays locked in place, and the table spins the next mold section right under it while the first section is being unloaded. No stopping. No waiting. That’s the kind of small, continuous gain that adds up to huge numbers fast.
I remember when we first installed our demo rotary machine at a medical device lab. They were making small plastic syringes with a tiny rubber seal insert. Their old machine required a separate operator to load each seal one by one between cycles—add that labor time, and their cycle per part was 45 seconds. With the rotary table, half the mold stations were dedicated to the seal loading and the finished part ejection. The machine would spin the mold into place for injection, then immediately spin again to unload the finished syringe and drop in the next seal—all while the injection unit was already primed. Their cycle dropped to 22 seconds, and they didn’t need a full-time operator just for inserts anymore. That’s not just efficiency—that’s eliminating a whole step that was dragging them down.
Another big one: cycle time consistency. Let’s be real, old molding machines can be finicky. Temperature shifts, pressure dips, even operator fatigue can throw off cycle times, leading to parts that are flawed or take longer to make. Rotary table machines are built with precise, servo-driven rotation—no guesswork, no slow, jerky movements. The table spins at the exact same speed every single time, so the time between injection, cooling, and part removal is totally predictable. That means you can schedule production way more accurately, less downtime for reworks because of inconsistent cycles, and way less scrap.
Wait, scrap is another huge cost no one talks about. If a standard machine has a hiccup mid-cycle—like, say, the ejector pin sticks—you have to stop the whole press, clear the part, clean the mold, and that can mess up the rest of the batch. On a rotary table, if something goes wrong on one station, the other stations keep running. You don’t have to shut the whole machine down for a single issue. It’s like if your oven had multiple racks—if one rack has a burnt cookie, you still take the good ones out and keep cooking, instead of turning off the whole oven for one bad cookie. We had a customer making plastic phone cases a few months back, and their old press would scrap 7% of parts a week from cycle errors. After switching to a rotary, their scrap rate dropped to under 2%, just because they didn’t have to pause the whole line for a small station issue.
Energy use too—let’s not sleep on that. Everyone’s looking to cut utility costs these days, and rotary machines are way more efficient there. Standard molding machines have to heat up the whole platen every time it opens and closes, right? Every cycle, you’re heating, cooling, moving massive metal parts back and forth. A rotary table machine only moves the circular platen—way less mass to move, so less energy for motors and hydraulics. Plus, since cycles are shorter, you’re running the machine less time to hit the same output. Our data shows that for similar production volumes, rotary machines use about 25-30% less energy than standard two-platen setups. That’s hundreds of dollars a month saved on electric bills, which adds up over the year. I had a customer in the packaging space tell us that switching cut their monthly energy bill by $1,200—money they could put into expanding their line instead of wasting on utilities.
Oh, and labor savings! Let’s be honest, manufacturing labor isn’t cheap, and good operators are hard to find. On a standard molding line, you might need one operator per machine just to unload parts, load inserts, and fix small issues. With a rotary table machine, a lot of those tasks are automated into the station rotation. You might only need one operator for two or three rotary machines, because they only have to check on the whole line every hour or so, not hover over one press all day. We had a small family-owned business that makes household plastic goods—they were running two shifts with three operators per machine. After switching to two rotary machines, they cut down to one shift with two operators total, and still hit the same production numbers. That’s not just saving on wages—it’s also reducing labor errors, since there’s less hands-on work happening each cycle.
Wait, but let’s make sure we’re not just hyping these machines—they’re not perfect for every job, right? If you’re making super large parts, like a plastic bin that’s 3 feet wide, a rotary table might not have the platen size for that. But for small to medium parts—think medical components, auto clips, phone parts, packaging lids, anything that fits on a 12 to 24 inch platen—they’re a game-changer. The key is matching the machine to your product, not just buying the shiniest one. But for 80% of the small-to-medium batch production that’s out there? Rotary table is the move.
Another thing: flexibility. A lot of manufacturers have to switch between product runs all the time, and changing over a standard machine can take hours—adjusting platen alignment, reloading tooling, testing cycles. Rotary table machines make changeovers way faster because the stations are modular. You can swap out individual mold sections instead of the whole mold, so if you’re switching from making a soap lid to a pill bottle cap, you don’t have to take the entire platen apart. That means less downtime between runs, so you can take on smaller custom orders that big machines would waste time on. We had a customer who did custom plastic parts for local businesses—they used to turn down small jobs because changeover took too long. After getting a rotary table, they now do runs as small as 500 parts that make them extra profit, no hassle.
Let’s circle back to that production manager I was talking about at the start. He switched to a rotary table machine, and within three months, his output for those plastic clips went up 45%, his energy bill dropped 28%, and he only needed one operator instead of two for that line. He told me it was like “turning a broken faucet into a hose that actually fills the bucket.” That’s the real impact—these aren’t just machines with a fancy table; they’re built to eliminate the wasted steps that kill efficiency in every other molding setup.
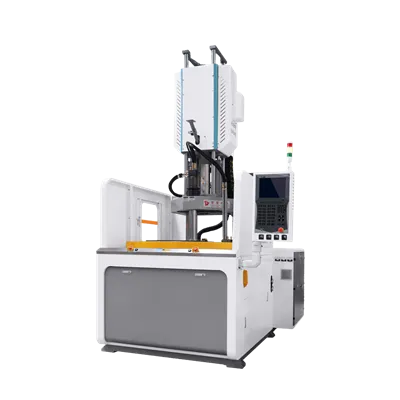
At the end of the day, if you’re tired of missed deadlines, high scrap, rising energy costs, and fighting to keep up with demand, a rotary table injection molding machine is the solution you’re probably looking for. We’ve worked with everything from startups to mid-sized manufacturers to get set up with the right machine for their specific parts and production goals, no one-size-fits-all garbage. If you’re ready to stop leaving money on the table and start cranking out more parts with less hassle, reach out to connect for a custom quote or to chat through your current production pain points.
Vertical Silicone Injection Machine References:
- Rosato, D. V., & Rosato, M. G. (2000). Injection Molding Handbook. Kluwer Academic Publishers.
- Manufacturing Engineering Society International Conference (MESIC). (2021). Efficiency Analysis of Rotary Table Injection Molding Systems.
- Plastics Technology Magazine. (2022). Energy Savings in Injection Molding: Comparing Rotary and Standard Press Designs.
- Society of Plastics Engineers (SPE). (2020). Rotational Molding and Rotary Table Molding: Process Optimization for Production Speed.
Guangdong Baizan Intelligent Equipment Co., Ltd.
We are one of the most professional rotary table injection molding machine manufacturers and suppliers in China. We warmly welcome you to buy customized rotary table injection molding machine at competitive price from our factory. If you have any enquiry about pricelist and quotation, please feel free to email us.
Address: No.8, Jianye Road, Dahuai Town, Enping City, Jiangmen City, Guangdong
E-mail: wjx@baizanjx.com
WebSite: https://www.baizanplast.com/
